Storage tanks, reactors, and fermenters
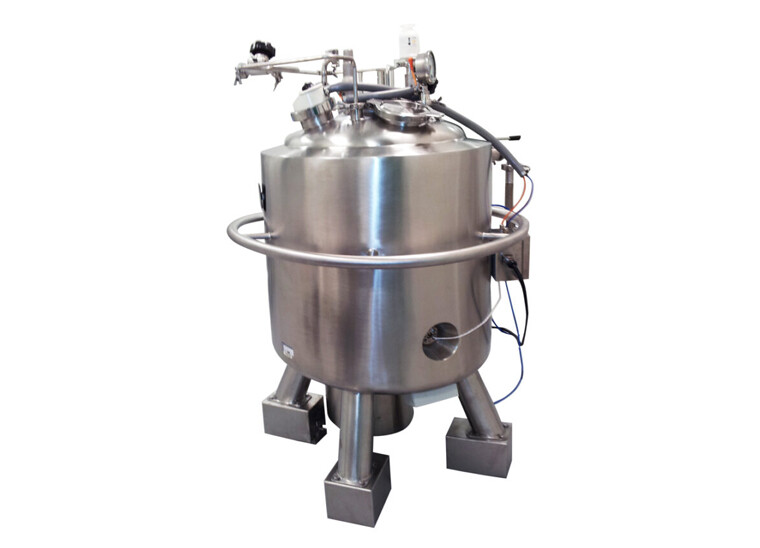
Neopure manufactures storage tanks, reactors, and fermenters for the pharmaceutical and biotechnology industries. We provide solutions tailored to each laboratory's specific needs, with capacities ranging from 50 to 15,000 liters. Options include pressure, atmospheric, and vacuum vessels; agitated or non-agitated units; and jacketed designs or those with heat exchangers.
Every project is unique, so we adapt to each user's specific requirements. The common denominator across our production reactors, tanks, and fermenters is the quality of materials and exceptional finish—featuring a surface roughness of ≤0.5 µm.
Custom Neopure Storage Tanks, Reactors and Fermenters for the Pharmaceutical and Biotechnology Industries.
Production area for solids, semi-solids, and liquids, as well as cleaning operations. Tanks and reactors are in continuous use in the pharmaceutical industry.
- Tank: AISI-316 L
- Shirt: AISI-316 L
- Piping, valves and instrumentation: AISI-316 L
- Bench: AISI-304
Neopure’s tanks, reactors, and fermenters are designed and manufactured according to each client's User Requirements Specifications (URS). They offer a wide range of options regarding materials (carbon steel, stainless steel, synthetic materials, fiberglass, etc.) and dimensions, as well as orientation (vertical or horizontal). They can be configured to withstand vacuum or pressure, and may include features such as jackets, heating, or cooling systems. Each design is tailored to the client's specific needs and intended functionality, with a multitude of optional features available, such as agitation systems and other variables.
Non-proprietary components (Gemü, Siemens, Festo, SMC)
If the project requires it, the equipment can be supplied fully certified and compliant with cGMP standards.
Storage tanks, reactors and fermenters for the pharmaceutical and biotechnology industries
Customized equipment from 50 to 15,000 litres, available in multiple configurations for pressure, vacuum, agitation, jackets and heat exchange, with high-quality sanitary finishes.
Would you like more information?
Tell us what you need and our team will get in touch with you.
PB VH2O2 Biodecontamination SAS
Cold PW and WFI generation systems
Pure steam generators